 EN
The Rising OPEX Burden in Industrial Water Treatment
In industrial water treatment, operating expenses are climbing due to tightening discharge regulations, aging infrastructure, and variable feedwater quality. Industry data from 2024 shows that OPEX for mid-scale membrane systems ranges from $0.36 to $1.20 per cubic meter treated, with energy consumption, chemical dosing, and membrane replacement as primary drivers. Membrane-based processes face escalating costs from fouling and frequent cleaning cycles. In power generation and chemical sectors, brine disposal fees have surged as zero liquid discharge mandates spread. Variable effluent composition further strains conventional treatment—pH, temperature, and pollutant swings cause separation failures that demand constant operator intervention and raise chemical use. At the same time, the retirement of experienced technicians and the high capital outlay for upgrades leave many facilities stuck with inefficient, OPEX-heavy setups. These interconnected pressures are pushing water-intensive operations to view treatment not just as compliance but as a critical lever for cost control.
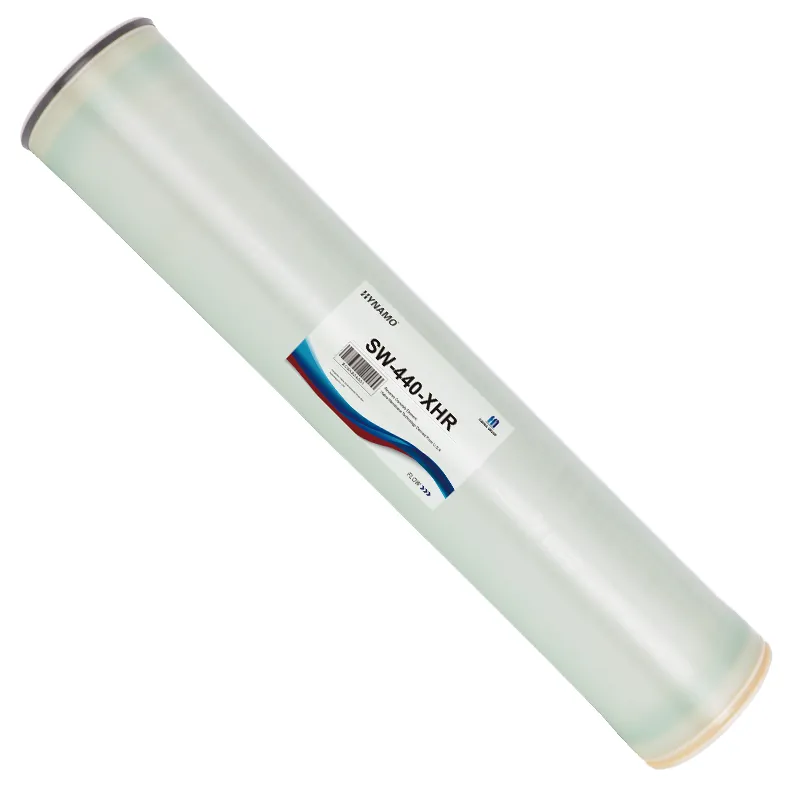
High Rejection Membrane Elements: Precision Engineering for Cost-Efficient Industrial Water Treatment
Core Performance Advantages: >99.8% NaCl rejection and stable flux at 15–25 bar
High rejection reverse osmosis membranes achieve over 99.8% sodium chloride removal, transforming brackish and saline feeds into high-purity permeate. This exceptional selectivity lowers total dissolved solids in the output, reducing downstream polishing demands and cutting chemical consumption for demineralization in boiler feed or electronics rinse water. The membranes maintain stable flux rates within a 15–25 bar operating window—avoiding the energy penalties of ultra-high-pressure systems while still concentrating brine effectively. For large-scale plants, the combination of near-complete ion rejection and moderate energy input translates directly to fewer membrane elements needed to meet throughput targets and a leaner high-pressure pump array. Consistent permeate quality also simplifies process control, enabling stable recovery ratios without frequent adjustment—and thereby stabilizing overall operational costs.
Fouling Resistance and Longevity: Polyamide layer optimization and surface topography innovations
Fouling remains the dominant factor driving chemical cleaning cycles and premature element replacement. Advanced polyamide thin-film composite membranes incorporate a densely cross-linked active layer that resists adsorption of organic foulants while retaining high rejection. Surface topography innovations—including patterned or smoother membrane surfaces—reduce physical anchoring points for colloidal particles and biofilms, lowering antiscalant and biocide dosing requirements in industrial water treatment. Some designs introduce a neutral or slightly hydrophilic charge distribution to repel amphiphilic contaminants common in food and beverage wastewater. The result is a robust membrane that endures frequent chemical cleanings without significant performance loss, extending service life by 12–18 months compared to earlier-generation elements. Longer intervals between cleanings minimize downtime, reduce labor and chemical expenses, and sustain salt rejection above 99.8% even after thousands of operating hours—transforming membrane replacement from an annual fixed cost into a multi-year strategic investment.
Balancing Performance and Practicality: Addressing Trade-Offs in Real-World Industrial Water Treatment
When ultra-high rejection backfires: scaling risk, cleaning frequency, and brackish feed compatibility
Ultra-high rejection membranes (>99.8% NaCl rejection) concentrate ions near the membrane surface, sharply raising saturation indices for sparingly soluble salts. This intensifies scaling—particularly calcium carbonate or sulfate—when treating feedwater with moderate hardness. Consequently, clean-in-place (CIP) intervals often shrink by 15–20%, increasing downtime and chemical use. For industrial water treatment with brackish feeds (2,000–5,000 mg/L TDS), the energy penalty of operating at 15–25 bar rarely offsets the marginal gain in salt passage. A more balanced design—employing membranes with rejection around 97–99%—frequently sustains stable flux, lowers antiscalant demand, and maintains permeate quality without the excess cleaning burden inherent in mismatched high-rejection elements.
Proven ROI Across Industries: Quantifying Cost Savings in Power, Pharma, and Food Processing
US Midwest coal plant: 22% lower brine disposal costs and 14% reduced antiscalant use
A coal-fired power plant in the U.S. Midwest upgraded its industrial water treatment with high-rejection membrane elements, transforming OPEX through targeted efficiency gains. By replacing legacy membranes, the facility reduced brine disposal costs by 22% within the first operating year. The enhanced NaCl rejection—exceeding 99.8%—concentrated dissolved solids more effectively, shrinking reject volume and off-site hauling expenses. Simultaneously, the more selective polyamide layer lowered antiscalant consumption by 14%, as reduced scaling potential at the membrane surface permitted relaxed chemical dosing. These combined savings shortened the upgrade payback to under 16 months—demonstrating how precision membrane engineering delivers quantifiable returns in heavy-industry water loops without compromising throughput.
FAQ
What factors contribute to rising OPEX in industrial water treatment?
Rising OPEX is driven by tightening discharge regulations, aging infrastructure, variable feedwater quality, increased energy consumption, and chemical dosing requirements, as well as expenses related to membrane replacement and brine disposal.
What are the benefits of high rejection reverse osmosis membranes?
High rejection reverse osmosis membranes achieve over 99.8% sodium chloride removal, reducing downstream chemical costs and providing stable flux within a 15–25 bar operating range. They help improve overall efficiency and reduce operational costs.
How do advanced membranes resist fouling?
Advanced polyamide thin-film composite membranes feature a densely cross-linked active layer and innovative surface topography that resist organic foulants and scaling. This enhances longevity and lowers chemical cleaning requirements.
What are the potential downsides of ultra-high rejection membranes?
Ultra-high rejection membranes can increase scaling risks and shorten cleaning intervals, especially when treating feedwater with moderate hardness. They may also lead to higher energy consumption for brackish feeds.
What is the ROI of upgrading to high-rejection membranes?
Upgrading to high-rejection membranes can result in significant cost savings, such as reduced brine disposal expenses and lower chemical consumption. For example, a U.S. Midwest coal plant achieved a 22% reduction in brine disposal costs and 14% lower antiscalant use, with a payback period under 16 months.
Table of Contents
- The Rising OPEX Burden in Industrial Water Treatment
- High Rejection Membrane Elements: Precision Engineering for Cost-Efficient Industrial Water Treatment
- Balancing Performance and Practicality: Addressing Trade-Offs in Real-World Industrial Water Treatment
- Proven ROI Across Industries: Quantifying Cost Savings in Power, Pharma, and Food Processing
-
FAQ
- What factors contribute to rising OPEX in industrial water treatment?
- What are the benefits of high rejection reverse osmosis membranes?
- How do advanced membranes resist fouling?
- What are the potential downsides of ultra-high rejection membranes?
- What is the ROI of upgrading to high-rejection membranes?